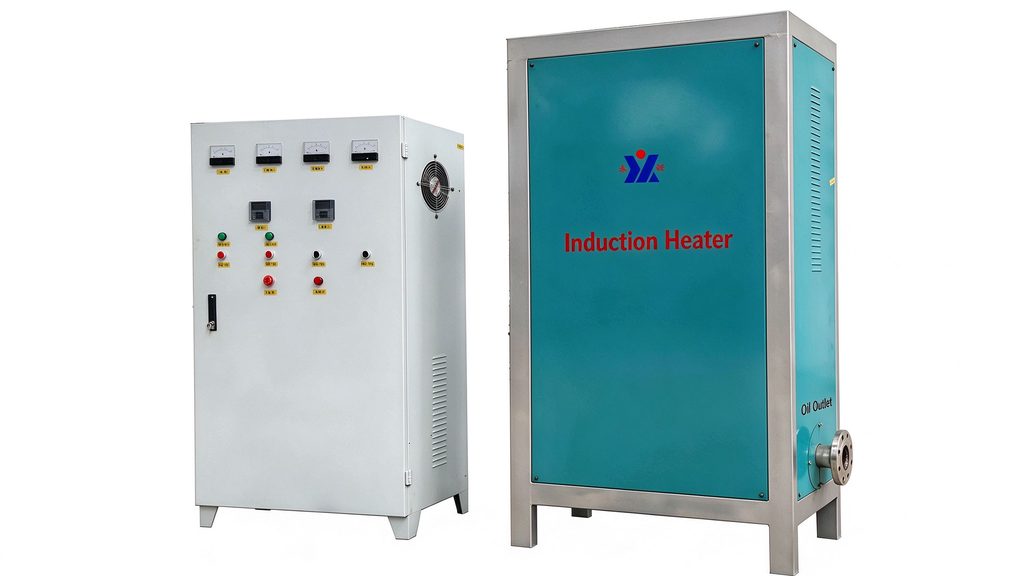
The induction thermal oil boiler features both cooling and heat recovery functions, with a wide load adjustment range and zero tar or wastewater discharge. It adopts high-temperature direct combustion technology, where tar and other byproducts are burned directly in gaseous form, eliminating secondary pollution. The fuel is fully combusted, delivering clear environmental benefits while saving energy.
Key Features:
- High energy efficiency: thermal efficiency reaches over 99%, consuming 30% less energy than conventional electric rod heaters under the same conditions.
- Lower maintenance costs: the induction heating cable is wear-free, eliminating frequent rod replacement and carbon buildup caused by high-temperature rod surfaces.
- Improved working environment: minimal heat loss, with the outer surface of the heating cylinder staying near room temperature.
- Isolated heating design: the induction coil heats only the cylinder wall, keeping it safely separated from the thermal oil. This eliminates fire risks from rod leakage and produces a magnetization effect on the oil to prevent carbon deposits.
- Fast start-up: preheating time is reduced by two-thirds compared to electric rod heaters.
- Fully air-cooled frequency converter and heating cable, requiring no water cooling system.
- Precise temperature control within ±1°C, capable of reaching up to 500°C where the thermal oil allows, meeting a wide range of high-temperature process requirements.